
 The complete production is performed with face hardening and deposition of anti-friction coating instead of imported parts delivery.Hard-face coating on the basis of tungsten carbide (hardness 70 HRC) is applied for face hardening, as anti-friction replacement for bronze coating БрАМц 9-2. Coating is applied by High Velocity Air-Fuel spraying processing. Finishegrinding is performed up to Ra 0,4µm.
 The refurbishment of piston-cylinder assembly is performed by reboring technique. Work performed:
– The refurbishment of geometrical dimensions is performed by anti-friction bronze coating in thickness 3 mm;
– Boring of cylinder housing for refurbishment of piston size.
– Refinishing surface roughnesses is Ra 0,8µm.
 The complete production is performed with face hardening and applying of coating on basis of tungsten carbide (hard-ness 70 HRC). Coating is applied by High Velocity Air-Fuel spraying processing. Finished grinding is performed up to Ra 0,4µm. Operating life of plungers is increased in 5-7 times in comparison with thermostrengthened steel (40X13) original.
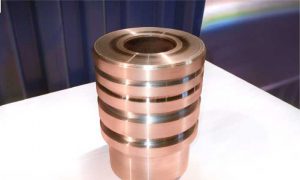 The complete production of steel workpiece is performed with applying of anti-friction coating in thickness 3,0 mm by wire flame spraying technique with subsequent grinding up to Ra 0,8µm.
 The refurbishment of abraded surface is performed with applying of anti-friction coating. Coating is applied by wire flame spraying technique with subsequent mechanical operation in accordance with drawing. Thickness of coating is 1,0-1,5 mm.
 Wear-resistance coating on the basis of tungsten carbide (hardness 70HRC) is applied on the working surface. Coating is applied by thermal spraying technique with subsequent grinding up to Ra 0,4µm. Thickness of coating is 0,4 mm.
 The complete production with face hardening is performed by hard-face coating on the basis on the tungsten carbide (hardness 70 HRC). Coating is applied by High Velocity Air-Fuel spraying processing. Finished grinding is performed up to Ra 0,4µm. Thickness of coating is 0,2 mm.Plunger have worked 650 hours free from wear instead of 500 hours.
 Plunger of high pressure three-throw plunger pump SIGMA PUMPV HRANICE (Czech Republic) (petroleum exploitation by spattering). The complete production with face hardening is performed by hard-face coating on the basis on the tungsten carbide (hardness 70 HRC). Coating is applied by High Velocity Air-Fuel spraying processing. Finished grinding is performed up to Ra 0,4µm. Thickness of coating is 0,2 mm.
 The refurbishment of abraded surface is performed with applying of anti-friction coating in thickness 5,0 mm on the working surface of piston (diameter 280 mm). Coating is applied by wire flame spraying technique. Finished grinding is performed up to Ra 0,8µm.
 The refurbishment of rod of hydraulic cylinder 2700 mm length, f 100 mm is performed with hardening and applying of wear-resistance metallized coating. Coating is applied by wire flame spraying technique. The hardness of coating is 48-50HRC. Durability is increased in 2-2,5 times.
 The refurbishment is performed with hardening of surface 1090 mm length, f 657 mm.Wear-resistance steel coating is depoisited with applying of powdery PPM6-1 (hardness of deposited coating 50-52 HRC). Coating is applied by wire flame spraying technique with subsequent polish up to Ra 0,2 µm.
 The refurbishment of rod of hydraulic cylinder is performed with hardening by and applying of wear-resistance metallized coating (hardness 48-50 HRC) in thickness 1,0-2,5 mm.Coating is applied by wire flame spraying technique. Finished grinding is performed up to Ra 0,4µm.
